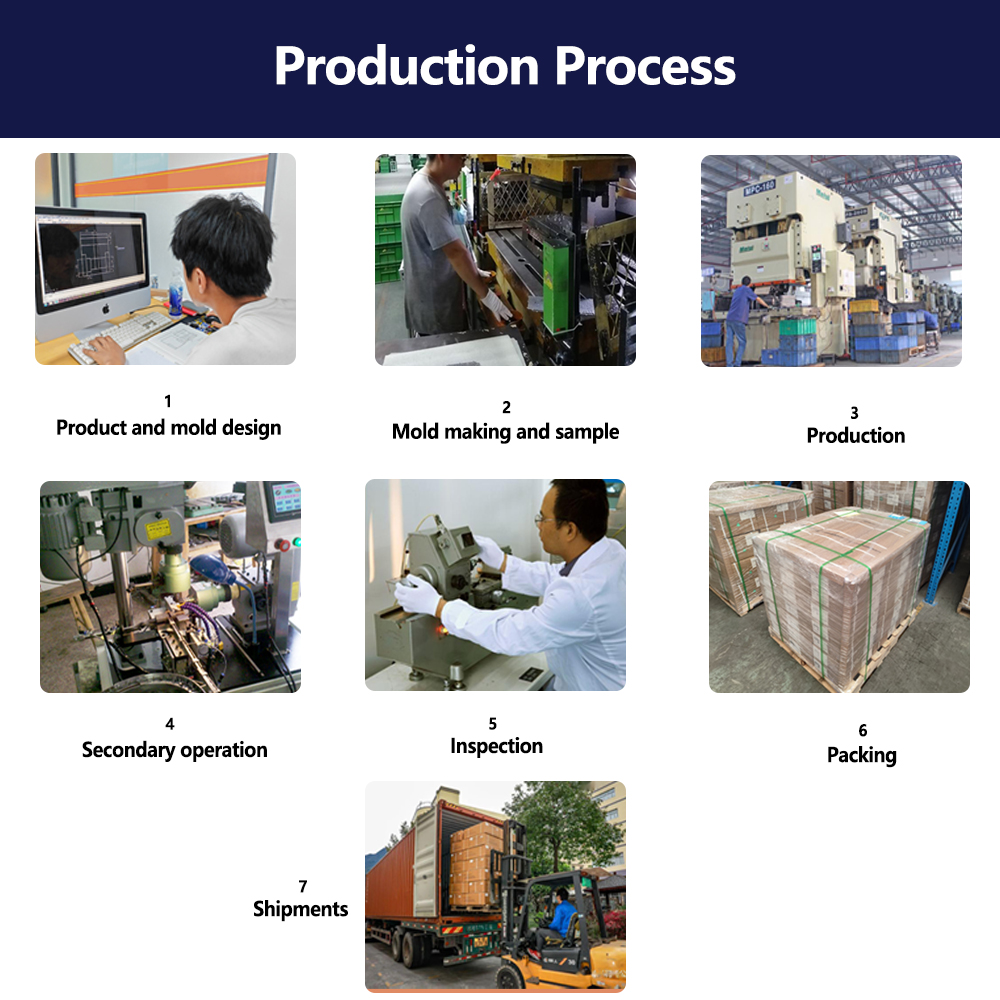
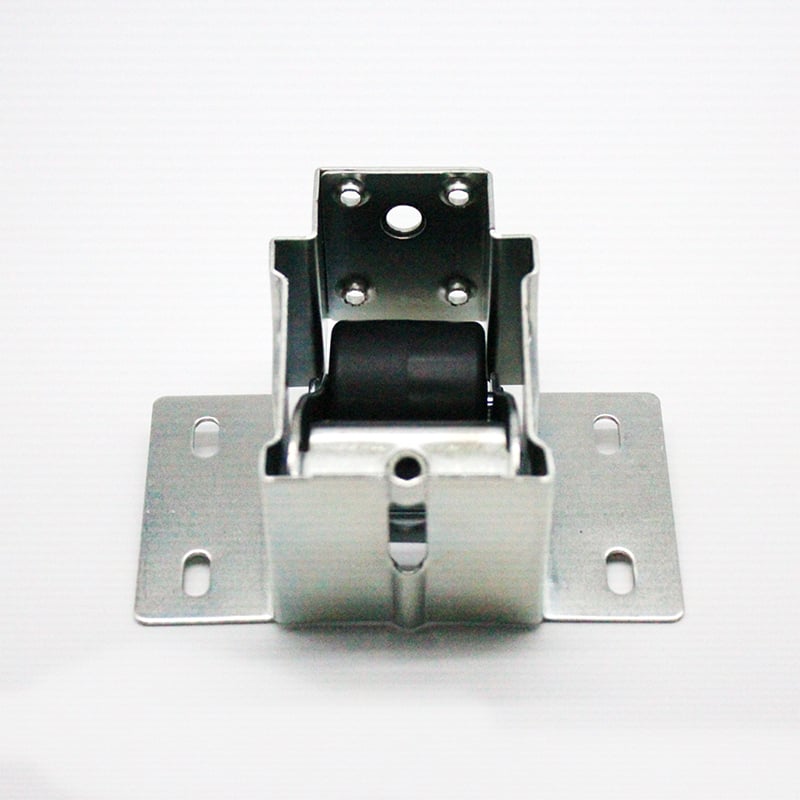
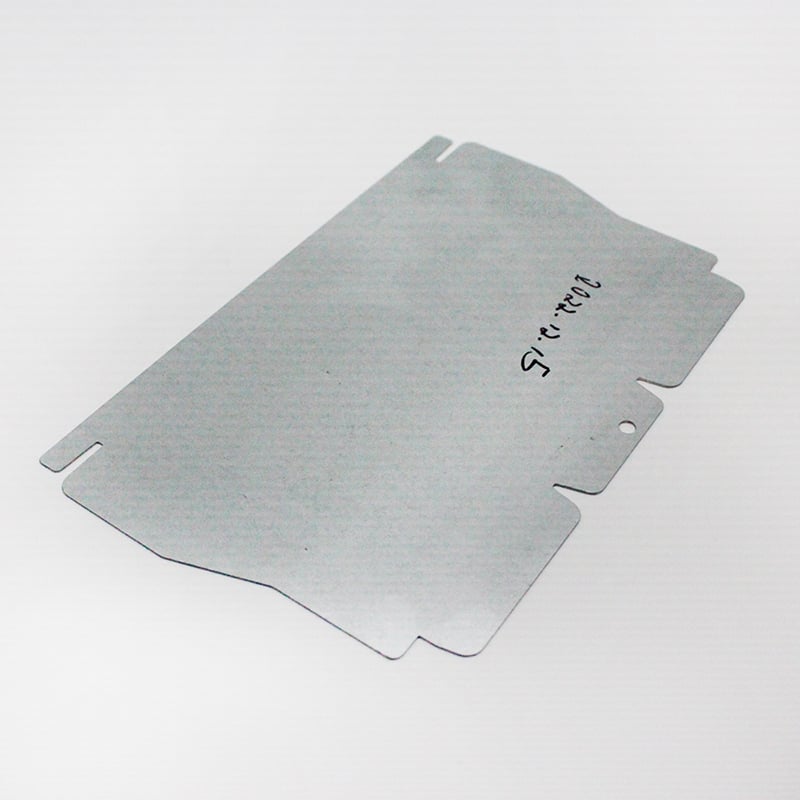
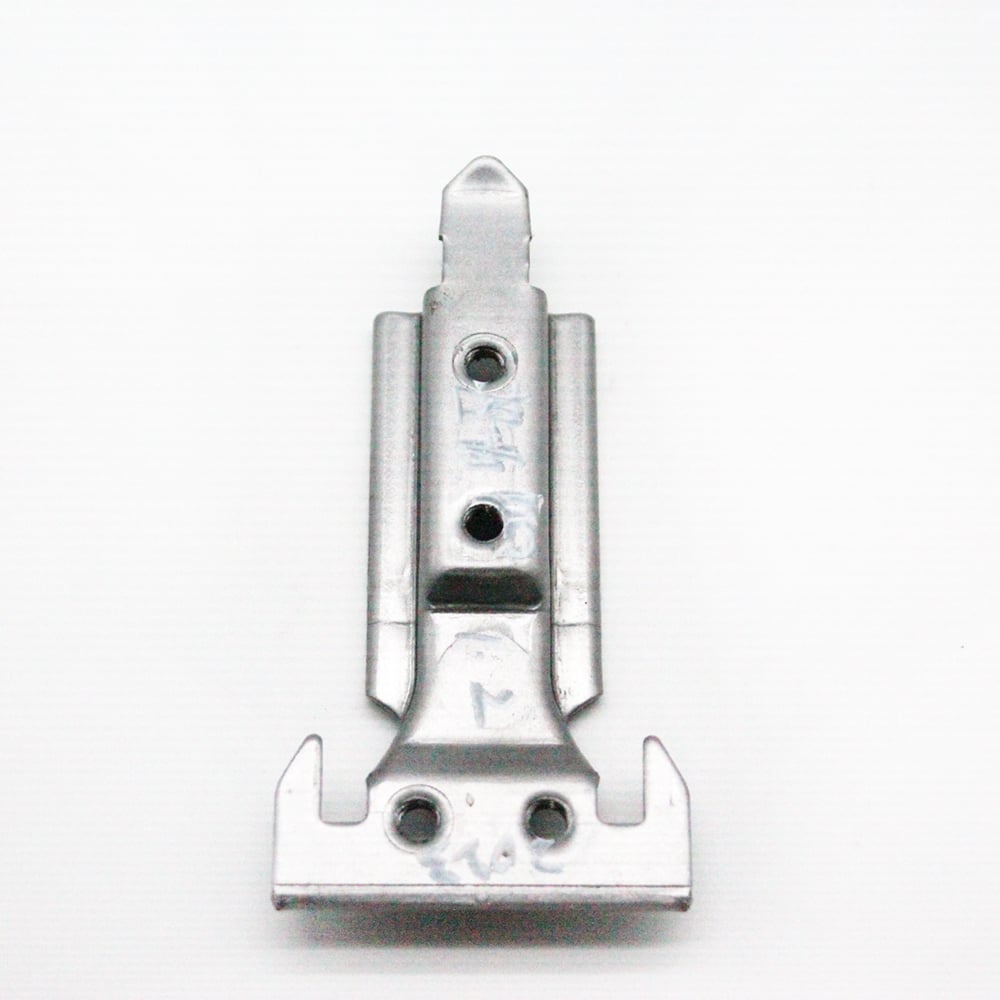
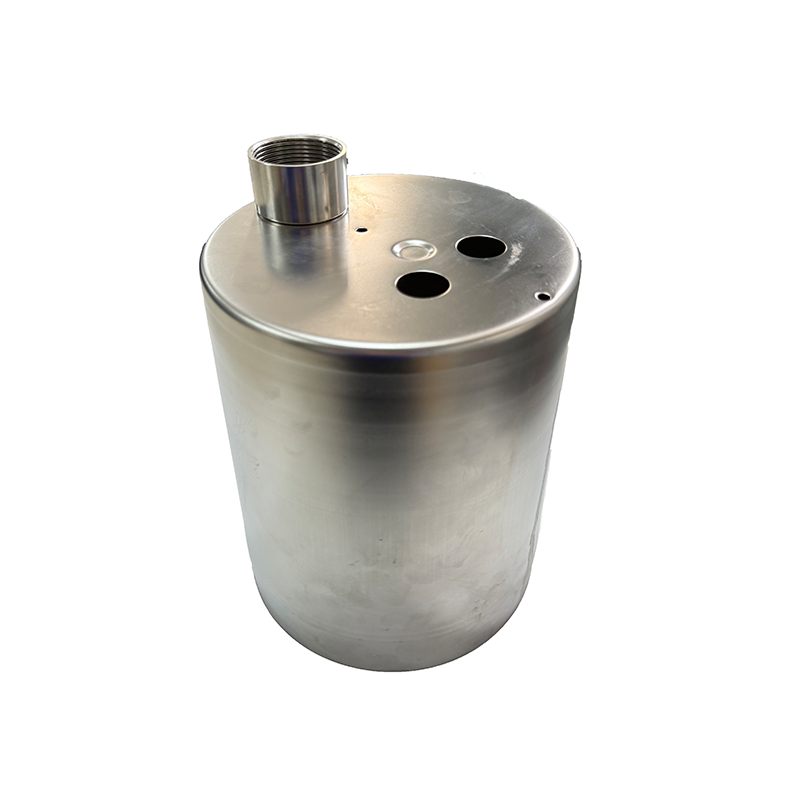
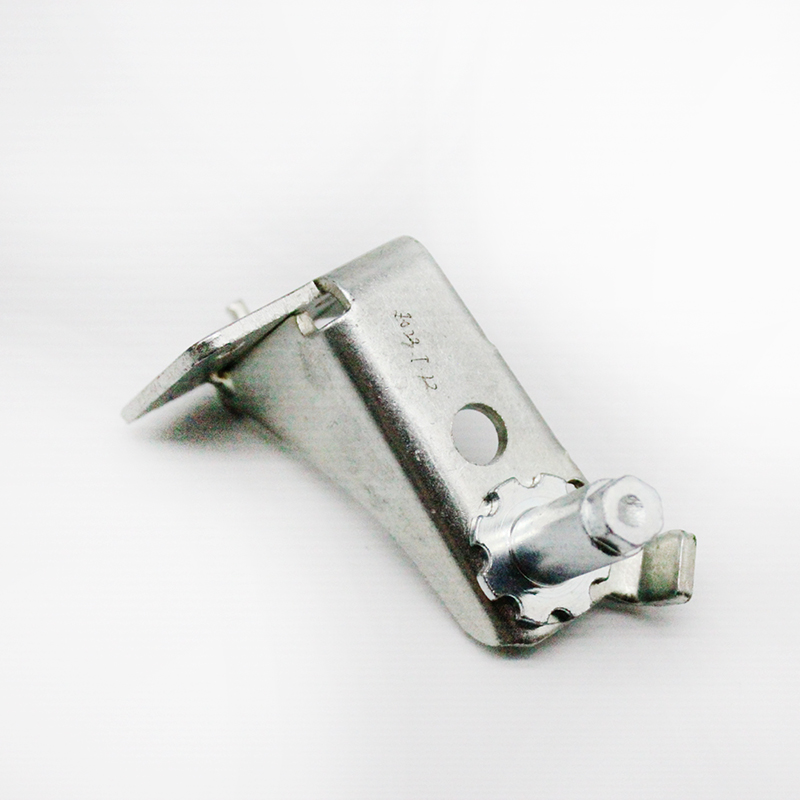
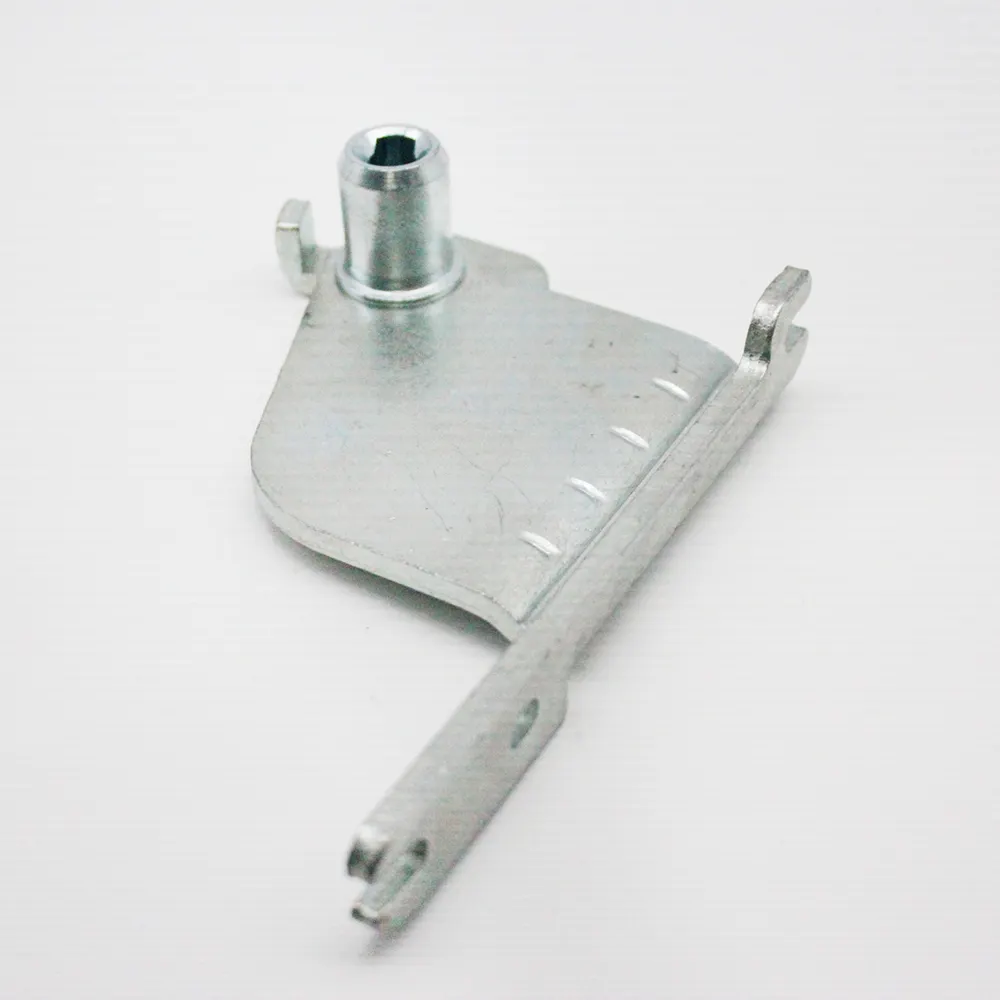
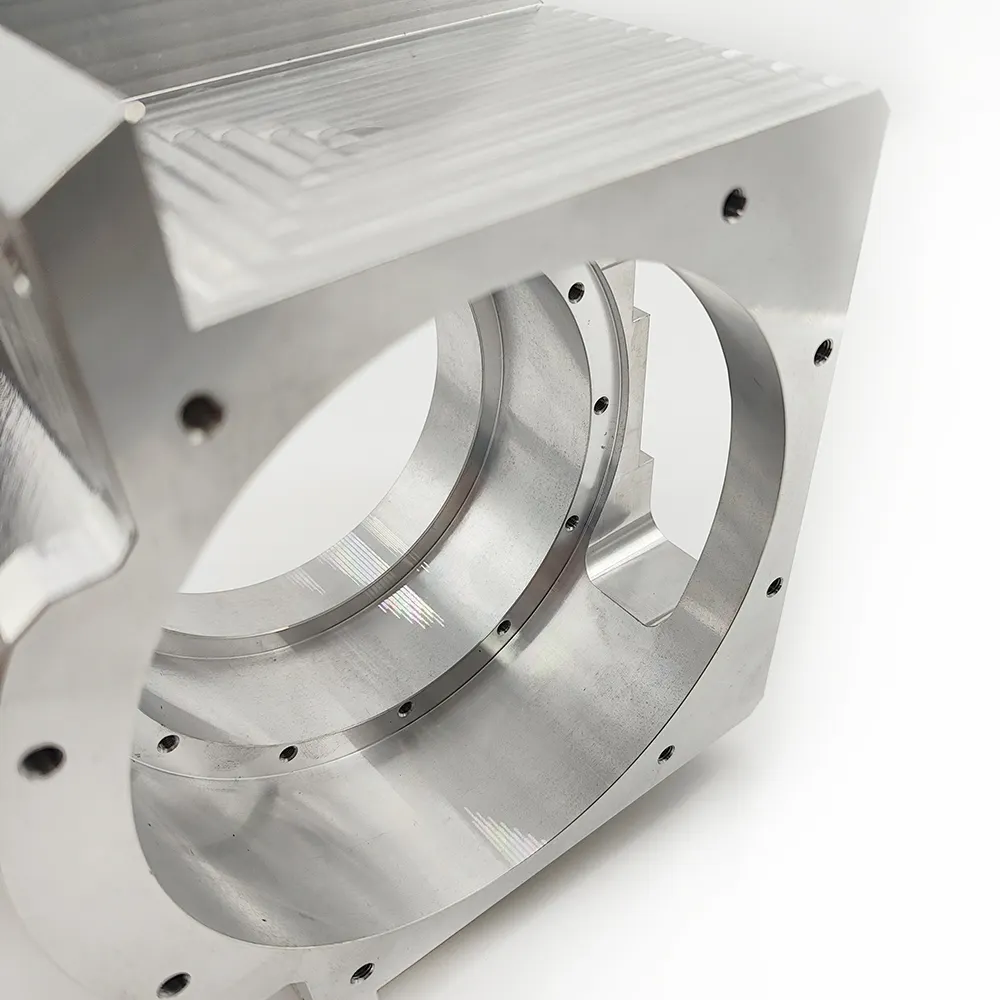
Since 1998, HRB Industries Corporation has been one of the leaders in the custom metal fabrication industry, earning a reputation built on careful detail, unwavering attention, and complete devotion to customer satisfaction. We combine the timeless artistry of old-world metal craft techniques with the precision and speed of new-world technological advancements, creating a manufacturing approach that is both innovative and deeply rooted in proven practice.
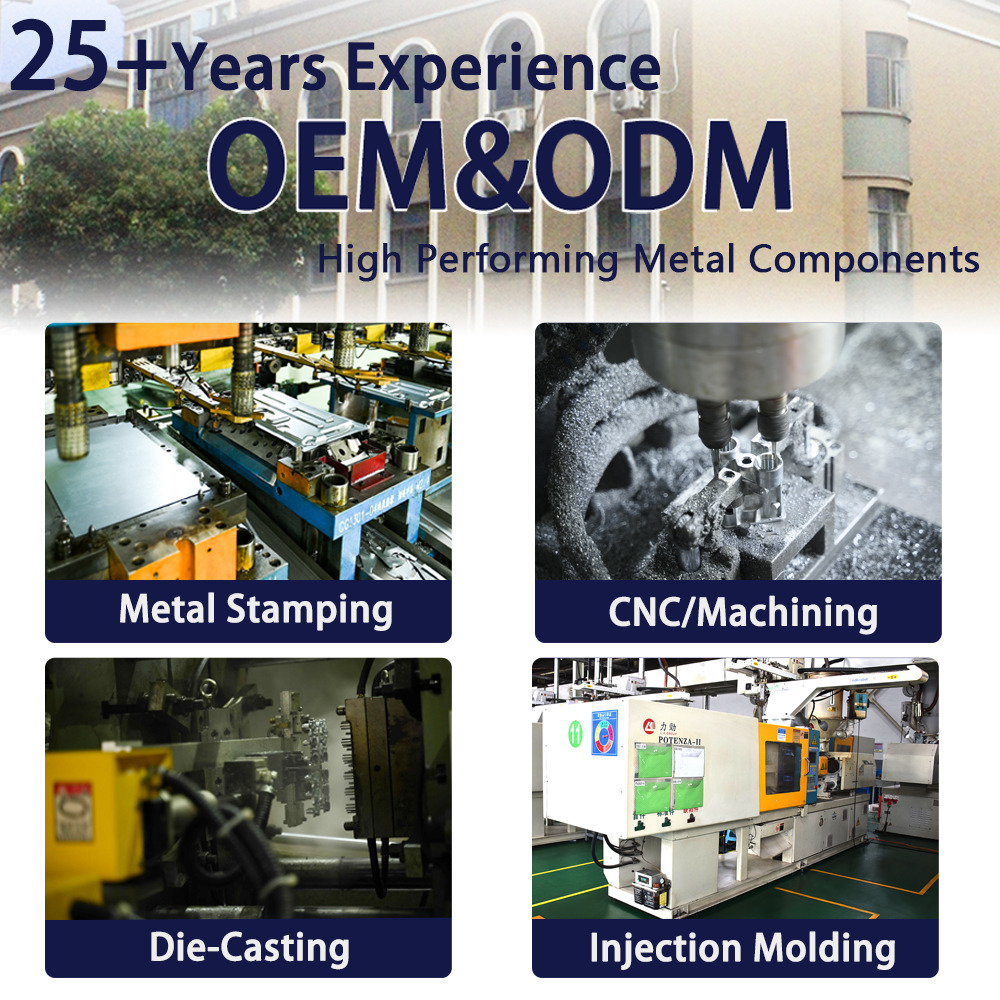
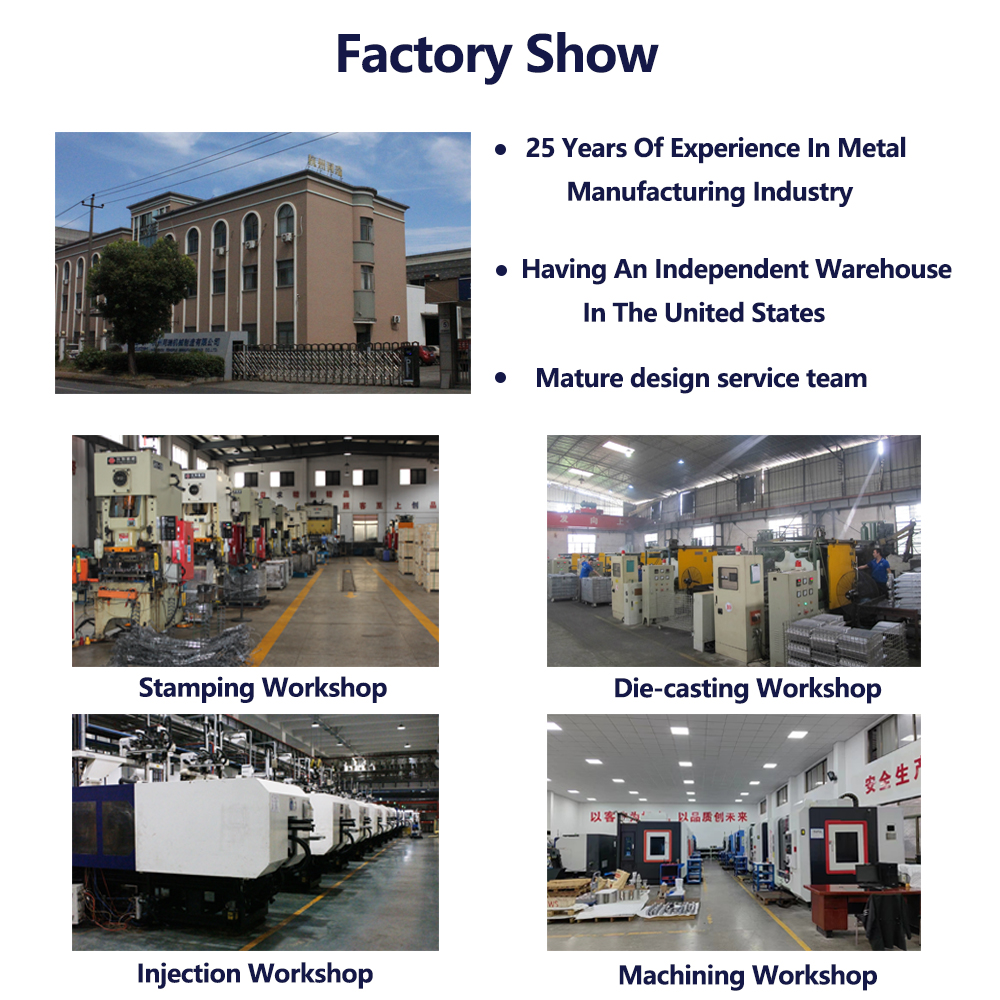
Our comprehensive manufacturing capabilities encompass a wide range of functions, including but not limited to sheet metal fabrication, precision CNC machining, metal casting, post-processing, and final assembly. This extensive in-house expertise makes us far more than a one-stop shop—it gives us the competitive advantage of operational efficiency and significantly lower production costs, benefits that we pass directly to our customers. By controlling every stage of production under one roof, we eliminate the delays, communication gaps, and quality inconsistencies that often arise when coordinating multiple external suppliers.
In recognition of the critical importance of reliable supply chains, we initiated our U.S. warehouse program in St. Charles, Illinois, in 2003. This program services our North American customers with high-volume demand and supply, ensuring rapid order fulfillment and significantly reducing lead times. It also eases logistical burdens, allowing our clients to focus on their primary business objectives without the distractions of inventory management or supply chain disruptions.
Our engineering team, composed of top talent from around the world, is singularly focused on product design and seamless process integration. They work collaboratively with clients to optimize every aspect of design and manufacturing, ensuring that our customers receive the best possible value for their investment. Through value engineering, material optimization, and process refinement, they consistently deliver solutions that balance performance, cost, and manufacturability.
Quality is embedded in every facet of our operations. Our Black Belt QA team implements top-level quality design and control systems, ensuring that every finished product is free from defects and meets the most stringent specifications. As an ISO 9001:2008 certified company, HRB Industries takes quality as one of the most important principles guiding all business functions—from initial customer consultation to final shipment. We are committed to delivering excellence in every product, every process, and every partnership.
 EN